How to Evaluate Material Handling Equipment Suppliers
Material handling equipment covers everything that moves, stores, and stages goods inside a facility, from a lift that gets pallets between floors to the trolley that carries them the last ten metres to the line. When you’re comparing material handling equipment for a new site or an expansion, the question isn’t just which single machine you need. It’s whether one supplier can engineer the whole chain of movement around your actual floor plan.
The Trigger Is Rarely One Machine; it’s a Floor Plan That Stopped Working
A new site goes live, a mezzanine gets added for extra storage, or a production line expands onto a floor your current setup wasn’t built to serve. The problem shows up in different places at once. Pallets pile up at the base of a staircase because there’s no safe way to get them to the level above. Racking that made sense a year ago no longer matches how inventory actually moves. Operators are carrying components by hand across distances a trolley should be covering. None of these are separate problems with separate vendors. They’re symptoms of a material flow that was planned around the old floor, not the one you’re running now.
Getting Goods Between Floors and Across the Facility
Vertical movement and horizontal movement solve different parts of the same problem, and we manufacture for both.
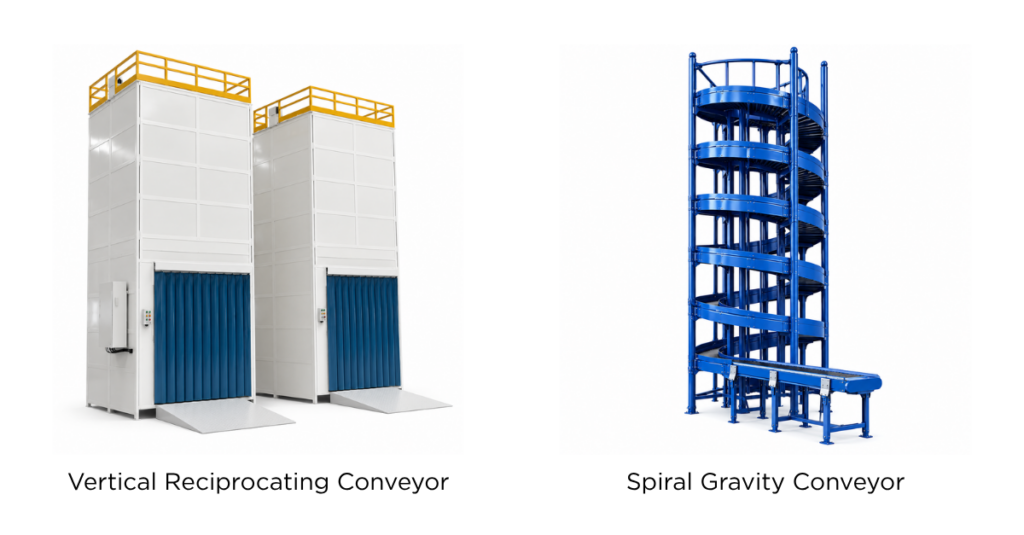
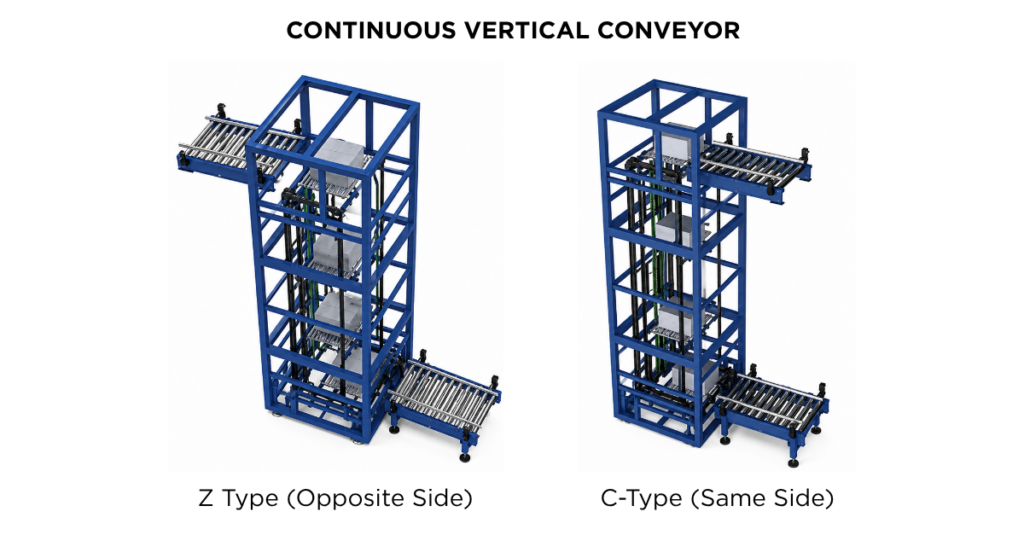
Our Vertical Reciprocating Conveyor (VRC Lift) moves material from one floor to another with high safety, and because it doesn’t need a dedicated machine room, it fits into sites where a passenger-style lift simply won’t. Our Material Handling Conveyors range covers the horizontal and inclined side of the same challenge, including Spiral Gravity Conveyors for continuous vertical descent that needs no power to run and Continuous Vertical Conveyors (CVC) for high-throughput movement between floors at a steady speed. Between the two, a facility can move goods from dock to floor and floor to floor without a manual carry anywhere in the sequence.
Storing, Staging, and Moving Goods Once They’re on the Floor
Getting material to the right level is only half the job. What happens once it’s there depending on how it’s stored, staged, and shifted from station to station.
- Pipe & Joint System: modular storage racks and warehouse racking, easy to assemble and reconfigure without the fabrication delays of a welded structure
- Industrial Trolleys: wheeled units for the swift, easy movement of items between workstations, storage, and dispatch
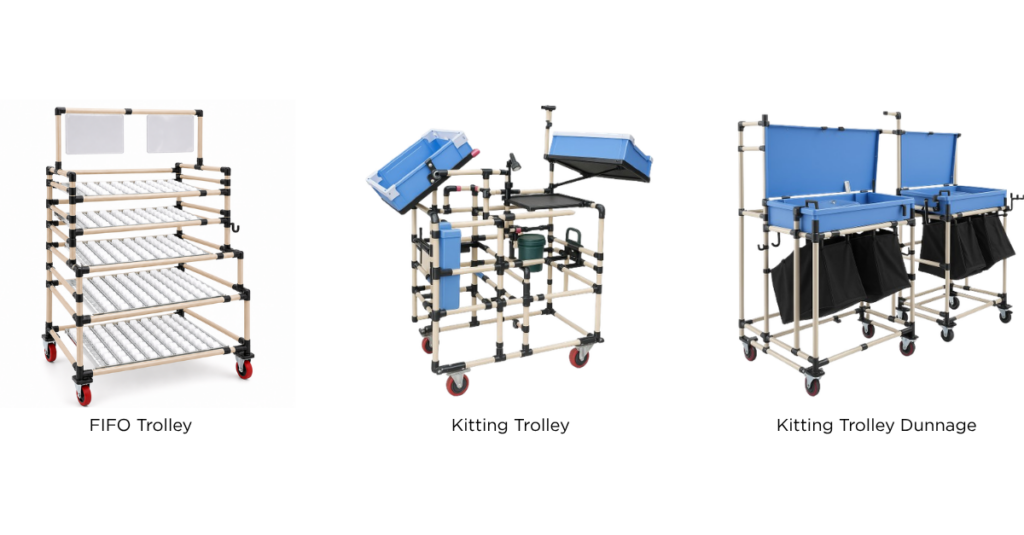
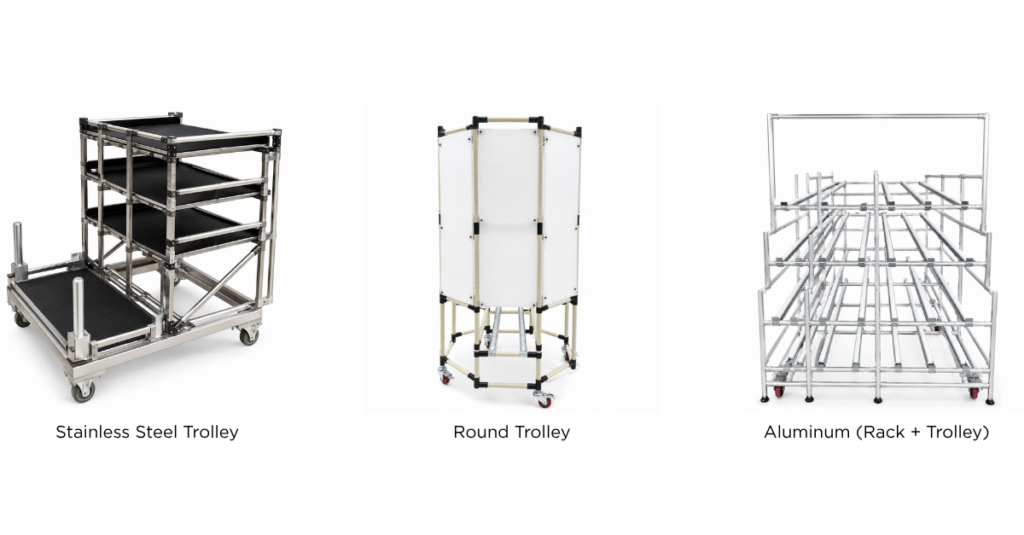
Each of these gets specified around your actual layout and load, not pulled off a fixed catalogue. A rack that’s easy to reconfigure matters less if the trolleys feeding it can’t handle the load, and both only work if they match how your VRC or conveyor line hands material off to them. Treating these as one connected system rather than separate purchases is where a lot of the wasted floor space and bottlenecks in a new site actually get solved.
Why It Matters That Your Supplier Is Expert and Trusted
A reliable supplier isn’t just about delivering equipment it’s about standing behind it. When you choose an expert manufacturer with proven installations, you gain more than machinery. You gain a partner who understands floor conditions before quoting, and who can send trained support on call or in person whenever needed. That level of trust means fewer surprises after handover, faster resolution if something needs attention, and confidence that your investment is backed by experience.
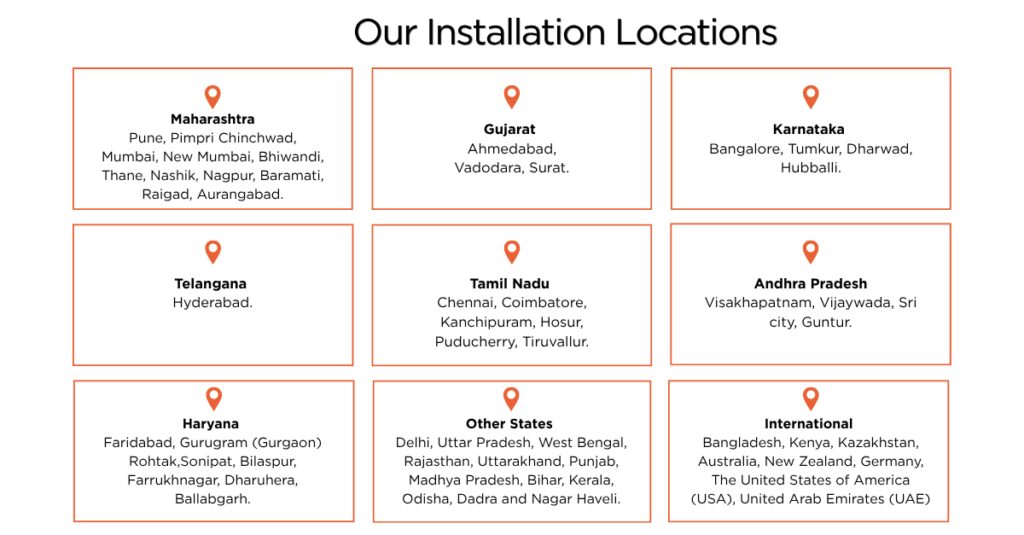
If you’re comparing material handling equipment suppliers for a multi-site rollout, working with one supplier who understands VRCs, conveyors, racking, and trolleys as parts of a single system, rather than separate vendor relationships, tends to keep both the installation timeline and the service relationship afterward simpler.
We’ve been manufacturing material handling equipment since 1998, and we’re an
ISO 9001:2015 certified manufacturer with over 1000 installations completed across the country to date. Every system we build, whether it’s a single VRC or a full site fit-out across our product range, is engineered around the load, layout, and workflow of the facility it’s going into.
Talk to Us Before Your Site Layout Is Finalized
The earlier we’re involved in a new site or expansion plan, the more flexibility you have on how vertical lifts, conveyors, racking, and trolleys work together on your floor. If a floor plan on your site isn’t keeping up with how material actually needs to move, we can walk through it with you before the civil work gets locked in.
Contact us to know more: Phone: +91 7774020056
Email: sales@technovisionengrs.com Website: www.technovisionengrs.com
Tags: material handling equipment manufacturers, material handling equipment manufacturers in Maharashtra, material handling equipment suppliers, material handling equipment suppliers in Maharashtra, material handling equipment suppliers, material handling equipment manufacturers in Pune, material handling suppliers in Pune, material handling lift, material handling conveyors, pipe and joint system, material handling solutions, material handling equipment manufacturers in India, material handling equipment suppliers in India, material handling trolley, material handling racks, material handling conveyors.